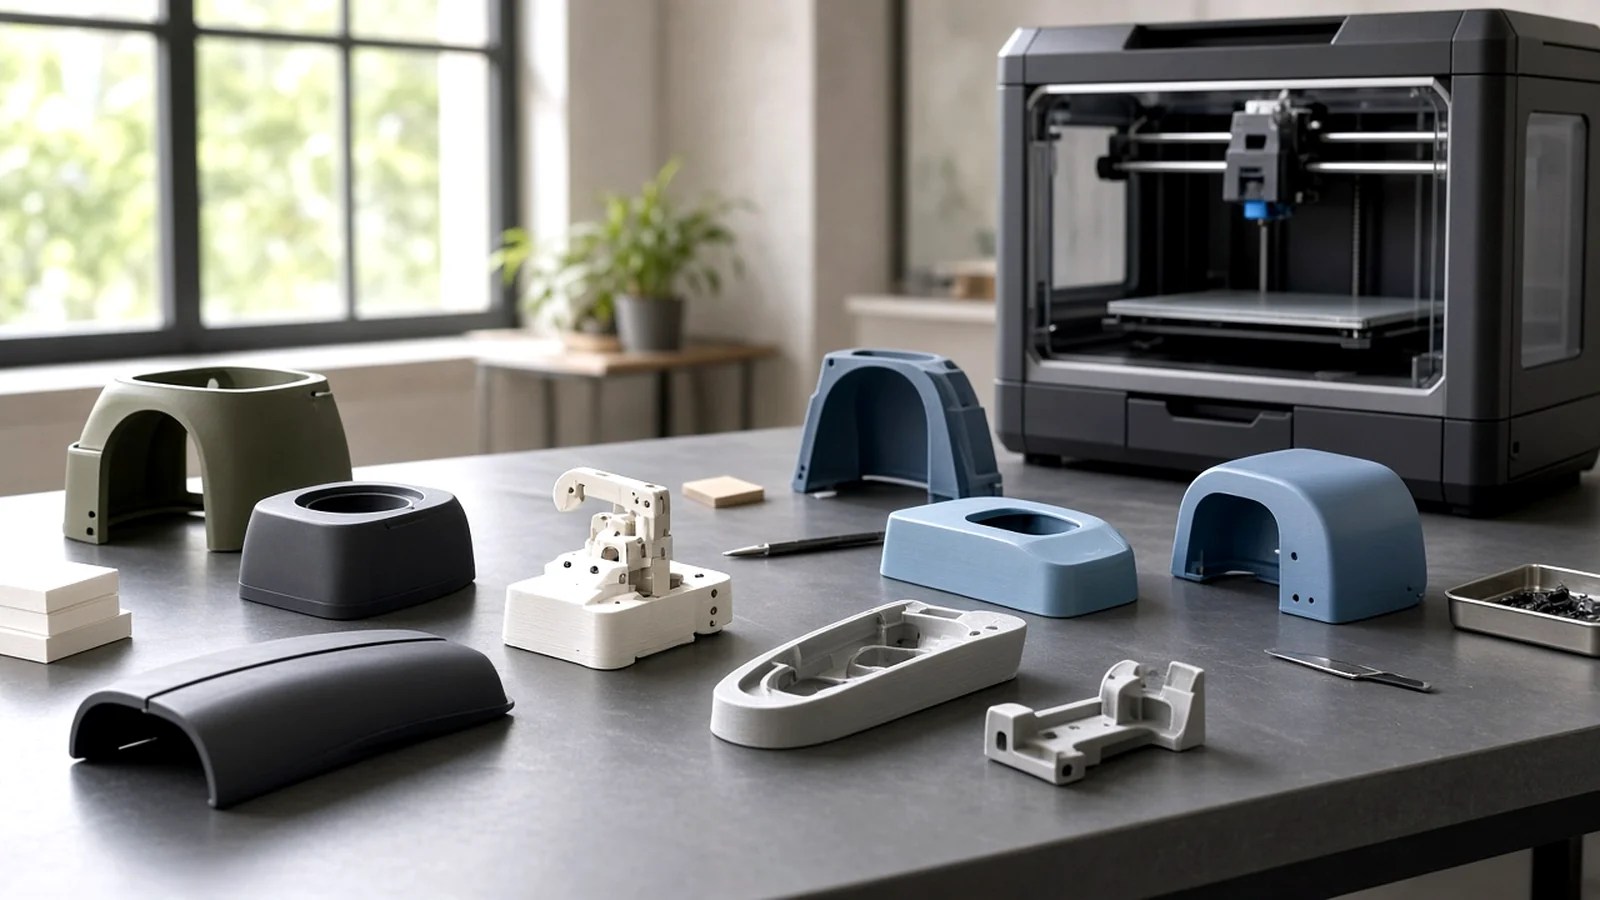
Hand boards (appearance and assembly prototypes) still drive design reviews. Industrial enclosed FDM replaces slow SLA farms and soft tooling when parts are large, painted, or need snap-fit iterations in days.
1. What “good enough” means for a hand board
- Stable dimensions after paint / plating prep
- Assembly clearances that match production intent
- Surfaces that sand and fill without melting
2. Why industrial enclosed beats desktop farms
- Chamber heat for ABS/ASA housings
- Larger envelopes on C9 / C12
- Repeatable jobs when marketing needs three colorways
3. When to switch to pellet FGF
Bulky mockups and packaging forms often cost less in FGF pellets; keep FDM for logos, thin walls, and living hinges. Hybrid shops run both — see FGF vs filament.
4. Buyer checklist
- Max part envelope and paint process
- Material (ABS/ASA vs PETG) and chamber need
- Weekly prototype count vs one show model
- Request a QS quote pack with your CAD envelope
Tags: industrial FDM printer, C6 FDM, C9 FDM, engineering filament, production 3D printing, 3D printed furniture, industrial 3D printing, FDM FGF LSAM, filament extrusion, medical 3D printing, sculpture 3D print, local filament factory, QS3Dmachine